

_500x500.jpg)
『Industrial Argon Flow Meter Calibration for Shielding Gas Control』Related information(flow rotameter|digital flow meter|balo meter|hydraulic flow meter|volumetric meter|positive displacement meter|pitot tube flow meter|displacement meter|cfm meter|variable area flow meter|inline flow meter|differential pressure flow meter|calibrated flow meter|velocity meter|paddle wheel flow meter|oval gear flow meter|anemometer hvac|multiphase flow meter|doppler flow meter|thorpe tube flowmeter|heat flow meter)
Industrial Argon Flow Meter Calibration for Shielding Gas Control
Quick Answer
Argon flow meter calibration for shielding gas control directly affects weld quality and gas cost in fabrication shops. A poorly calibrated meter can overfeed or underfeed argon by 15 to 30 percent without the operator noticing. Silver Instruments recommends annual field calibration with a portable reference meter or sending the unit to our lab. Share your DN, gas pressure, and flow range with our team and we will return a calibration certificate traceable to ISO/IEC 17025 within 5 working days.
Why Shielding Gas Calibration Slips Under the Radar
Most welding engineers focus on wire feed speed, voltage, and travel speed. The flow meter gets installed and then forgotten for years. In practice, a thermal mass flow meter or a variable area meter (rotameter) on an argon manifold can drift because of internal contamination, mechanical wear on the needle valve, or moisture ingress in the regulator. We have seen this on customer sites many times. A job shop in Thailand running GTAW on stainless steel pipe thought they had a porosity problem. After checking everything else, they sent us the argon flow meter. The calibration was off by 22 percent at 15 L/min. That 22 percent meant each weld used extra argon, and on a 12-month contract the overconsumption alone was worth more than three new meters.
Two Calibration Paths We Offer
Silver Instruments provides in-house lab calibration and on-site field calibration for argon and mixed shielding gas meters. The lab route suits new meters, annual recalibration schedules, and pre-delivery checks. We use a Fluke molbloc/molbox gas flow standard with a measurement uncertainty of ±0.2 percent of reading. Every meter leaves our Nanjing lab with a calibration certificate showing 5 test points (25%, 50%, 75%, 100%, and 125% of the span) and a linearity plot. Typical turnaround is 5 working days after we receive your instrument.
Field calibration works better for large manifolds, built-in flow meters on automated welding cells, or customers in remote industrial zones. Our service engineer brings a battery-powered reference thermal mass flow meter and a regulated argon cylinder to your site. The process takes about 20 minutes per meter. We compare the DUT against the reference at three flow rates, adjust zero and span if the meter allows it, then issue a field calibration report. Last year we did this for a shipyard in Batam, Indonesia, across 38 argon points on their panel lines. The crew did not need to disconnect a single fitting.
Which Meter Types We Calibrate
The calibration procedure changes a bit depending on the meter technology. Variable area meters (glass tube and metal tube) are the most common in shielding gas applications. We inspect the float, the tube, and the valve seat before calibration because a scratched tube or a flattened O-ring invalidates the results. Thermal mass flow meters are simpler to calibrate but sensitive to gas composition. A customer in Mexico sent us a meter calibrated for pure argon; they later used it with an argon-CO2 mix without reprogramming. The reading error jumped to 18 percent. We now train distributors to ask about gas composition first. Coriolis mass flow meters can also measure argon and mixed shielding gas with direct mass output. These rarely drift but still benefit from a verification run against a known standard once a year. Oval gear meters and turbine meters appear less often in argon service, but we have the gas rigs for them too.
Calibration Points and Gas Match
Industrial argon flow meters for shielding gas normally operate between 5 L/min and 25 L/min for GTAW and GMAW processes. We recommend calibration at 5, 10, 15, 20, and 25 L/min. For laser welding applications that use 1 to 5 L/min, we adjust the range down to 0.5, 1, 2.5, and 5 L/min. Always calibrate with the actual gas or a
What to Send Us Before Calibration
Send us your pressure (bar), temperature (°C), pipe size (DN), and flow range. Also mention the gas type and whether the meter includes a built-in needle valve or regulator. This helps us prepare the right upstream pressure and connection fittings. For example, a DN15 variable area meter with a 1/4 inch NPT inlet needs a different adapter than a DN25 thermal mass flow meter with tri-clamp ends. Email [email protected] with these details and we reply with a quote within the same working day. If you have multiple meters, attach a simple spreadsheet with tag numbers and we handle the rest.
On-Site Calibration Kit We Deploy
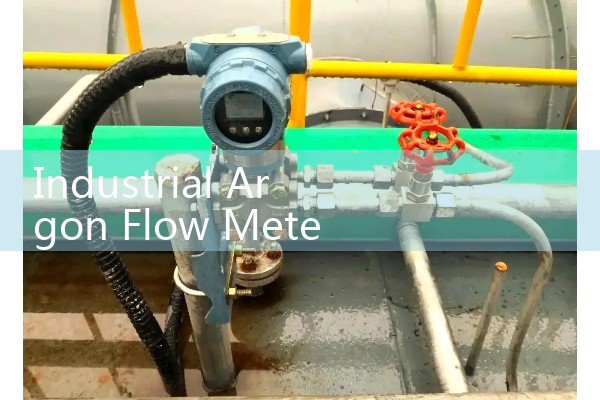
Our field kit for argon shielding gas contains a calibrated thermal mass flow meter as the transfer standard, a portable data logger, and a pressure reference module for upstream pressure verification. The reference meter itself is recalibrated every 6 months and carries a PTB-traceable certificate. We also bring a portable dewpoint meter to check for moisture in the argon supply because wet argon causes erratic flow readings on thermal sensors. This small check has caught valve leaks and regulator problems before they became weld defects.
Common Failures We Catch During Calibration
Zero drift is the number one issue. A meter reads 1.5 L/min when the actual flow is zero. This often happens in hot environments where the sensor electronics warm up unevenly. Mechanical zero adjustment fixes it on most variable area meters. Span drift is less common but more expensive to fix. A thermal meter that reads 18 L/min instead of 15 L/min at full scale usually needs a firmware correction or sensor cleaning. In rare cases, a damaged sensor element requires replacement. We always inform you of the as-found and as-left data before changing anything. You decide whether the error is acceptable or if repair is needed.
FAQ
Q: How often should I calibrate an argon flow meter for shielding gas?
A: Once a year for most welding applications. High-purity pipe welding or aerospace jobs may require calibration every 6 months. This matches ISO 3834 and AWS D1.1 recommendations for periodic inspection of welding ancillaries.
Q: Can I calibrate the flow meter myself with a portable reference?
A: Yes, if you have a calibrated reference meter with an up-to-date certificate. Many of our customers do this between our visits. We can supply a portable argon reference meter with data logging if you do not own one already.
Q: Do you calibrate meters from other brands?
A: Yes. We calibrate Brooks, Bronkhorst, Sierra, Fathom, and many Chinese domestic brands. Your meter does not need to be purchased from Silver Instruments.
Q: What is the cost?
A: A standard lab calibration for a single argon flow meter starts at USD 85 excluding shipping. Field service pricing depends on location and number of points. Request a quote by email with your site location.
Q: Do you offer turnkey packages with calibration included?
A: Yes. We sell argon thermal mass flow meters with a first calibration certificate included. Request a quote for meter plus calibration and we ship the unit ready to install.
Get in touch with Silver Automation Instruments to schedule your next argon flow meter calibration. Email: [email protected] | Tel: +86-135-1213-1526 | Whatsapp: 86-135-12131526 | WeChat: +86 13512131526. Visit our main site at flow-meter.com.au for more gas measurement solutions.
 Hot Product
 Related AD